About 180 Degree Modular Belt Conveyor
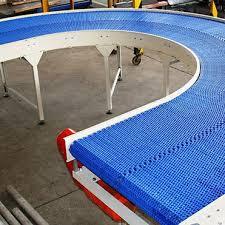
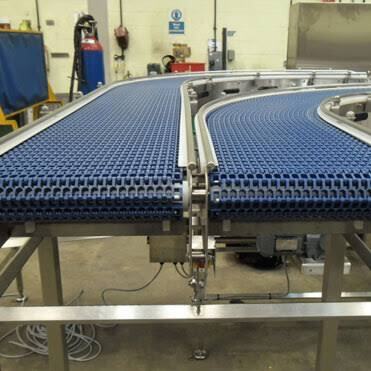
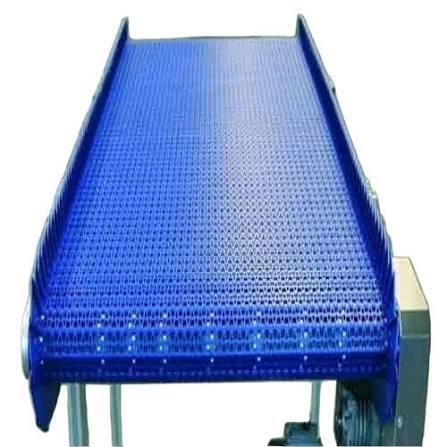
Uncommon in its build quality and famed for its dominant performance, our 180 Degree Modular Belt Conveyor is a rare find-order now as supplies are ending soon. Designed for demanding food, pharmaceutical, packaging, and warehouse environments, this belt conveyor boasts a corrosion and wear-resistant plastic modular belt, supported by a rugged mild steel or stainless steel frame. With customizable widths (300-1200 mm), frame height, angle, and drive types, it is engineered for high capacity (up to 200 kg/m) and reliable, low-noise operation. Its precision-machined idler rollers and easy washdown design ensure both efficiency and hygienic standards are maintained. Featuring easy belt replacement and minimal maintenance, this specialized conveyor is an optimal manufacturing and supply solution across industries in India.
Material Feature & Competitive Advantages
The 180 Degree Modular Belt Conveyor stands apart with its food-grade polypropylene modular belt, providing exceptional corrosion and wear resistance. Its powder-coated or polished mild steel or stainless steel frame ensures lasting durability even in demanding environments. Precision-machined idler rollers and a low-noise, high-efficiency drive system present uncommon advantages, making this conveyor the superior choice for industries requiring both hygiene and robust performance. Easy belt replacement and adjustable speeds round out its competitive edge.
Sample Availability & Certifications
Interested customers can request a sample via Purchase Order with our straightforward supply process. We facilitate convenient drop-off arrangements to demonstrate our conveyor's quality and function. Our 180 Degree Modular Belt Conveyors are supported by necessary certifications aligning with industry benchmarks, guaranteeing peace of mind on operational standards. Our sample policy ensures that buyers can confidently evaluate performance before committing to widespread implementation.
FAQ's of 180 Degree Modular Belt Conveyor:
Q: How can I customize the 180 Degree Modular Belt Conveyor to suit my facility?
A: You can tailor the conveyor's belt width, frame height, curve angle, and drive type to fit your unique operational needs. Discuss your requirements with our team for a made-to-order solution.
Q: What industries benefit most from the 180 Degree Modular Belt Conveyor?
A: This conveyor is ideal for food, pharmaceutical, packaging, and warehouse sectors, offering hygienic, durable, and efficient material handling tailored to strict industry standards.
Q: Where can the conveyor be installed and what installation support is provided?
A: Our conveyor is designed for secure floor mounting. We provide clear installation guidance and support to ensure safe and effective integration into your facility.
Q: What is the cleaning process, and how does the easy washdown design help?
A: The conveyor's easy washdown design enables quick, thorough cleaning-particularly vital in food and pharmaceutical industries-helping maintain hygiene and reduce downtime.
Q: When should I place an order if I require a sample before bulk purchasing?
A: To secure a sample and timely supply, it's best to submit your purchase order early, as availability is limited and orders are fulfilled on a first-come, first-served basis.
Q: How does the dominant performance of the conveyor improve operational efficiency?
A: With adjustable speed, high load capacity, precision rollers, and minimal maintenance, the conveyor streamlines workflows and reduces operational downtime, driving overall productivity.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
